


Custom left hand thread hex nut Factory: What Buyers Should Check Before Ordering
Fatigue appears at the stress concentration when a nut runs with uneven thread engagement, excessive preload or a poor fit with its mating fastener. For a procurement officer qualifying a second source, the key question is whether each production lot holds the same thread direction, fit and geometry—not simply whether the quotation matches the drawing.
What the Design Has to Balance
Nut mass and section stiffness compete with the space available for a wrench and the required thread engagement. A taller body can provide more engaged threads, but it may interfere with adjacent parts; a compact nut may fit the assembly while leaving less material around the threaded bore.
Left-hand thread direction is a functional choice, not a marking detail. It suits assemblies where operating rotation or movement could tend to loosen a conventional right-hand connection. Confirm the mating bolt’s handedness, pitch and fit before release, then set the nut dimensions around the actual joint load and available tool access.
Construction Method and Its Effect on Consistency
For production runs suited to cold forming, the hex body is formed from wire or rod stock and the left-hand internal thread is tapped afterward. The tap direction and thread gauges must match the specified left-hand pitch; a right-hand thread tool or an incorrectly identified gauge can produce parts that look correct but will not assemble.
Cold heading supports repeatable body dimensions at volume, while tooling condition, stock variation and tapping setup affect lot-to-lot results. Buyers qualifying a second source should request confirmation of the forming route, in-process checks and how the factory separates left-hand parts from visually similar right-hand production.
A practical inspection plan checks across-flats size, nut height and thread fit with left-hand GO/NO-GO gauges at a defined sampling frequency. If a protective coating is specified, verify the thread fit after finishing as well; coating buildup can tighten the effective clearance and cause assembly failures even when the bare nut passed inspection.
Specification Range and Customisation Limits
| Specification | Typical order basis | What to confirm |
|---|---|---|
| Thread | Metric or inch series; left-hand direction; specified pitch | Thread class or fit, mating fastener and gauge acceptance criteria |
| Body dimensions | Across flats, nut height, chamfer and bearing-face details to drawing | Tool clearance, joint stack-up and the tolerance limits that affect assembly |
| Material | Carbon steel or stainless steel, subject to forming and service requirements | Required strength, corrosion exposure, heat treatment and mating fastener material |
| Finish | Uncoated or specified protective finish, subject to the drawing and service environment | Coating coverage, thickness where controlled, and final thread-gauge fit |
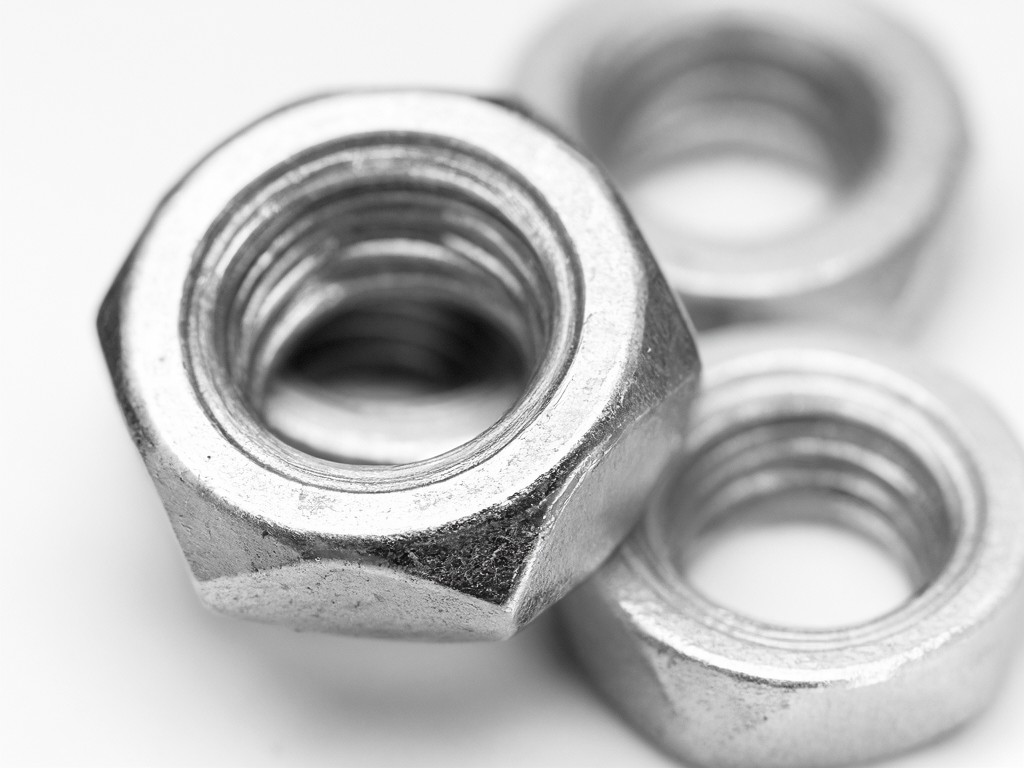
The limiting factor is rarely the headline specification. A non-standard pitch, unusual across-flats dimension or tight post-coating fit can require dedicated taps, forming dies or additional inspection. Send a controlled drawing with units, revision level and acceptance limits so a second-source quote reflects the actual production route rather than an assumed stock equivalent.
Buying Mistakes That Lead to Returns
Lowest Unit Price
A lower quote can omit the inspection effort needed to confirm handedness, thread fit and finish condition. If assembly rejects or warranty claims follow, the unit saving can be outweighed by sorting, freight and replacement costs.
Controlled Batch Cost
A documented gauge plan and lot identification add process cost, but they help isolate a deviation before it reaches the assembly line. Compare quoted inspection scope and replacement terms alongside price per piece.
Common order errors include:
- Listing a thread size without stating left-hand direction or pitch.
- Approving a sample before checking fit with the production mating bolt and the specified finish.
- Leaving material, strength requirements or drawing revision open to interpretation between purchase orders.
- Accepting mixed or unmarked lots without a traceable link to the inspection record.
For repeat OEM or private-label orders, retain the approved sample reference, drawing revision and agreed inspection record together. That baseline makes changes in supplier, finish or tooling easier to review before a full batch ships.
Ordering, Tooling and Lead-Time Questions
Can an existing nut be used as the reference?
A sample can help identify geometry, but it does not establish hidden thread tolerances or material requirements. Provide the drawing and mating fastener details; treat a sample as the approved reference only after dimensional and assembly checks.
What affects tooling cost and lead time?
Non-standard body dimensions may call for dedicated forming dies, while thread size and pitch determine tapping-tool requirements. Lead time also depends on material procurement, finish processing, sample approval and the inspection plan.
How should a second source be qualified?
Start with a production-representative sample and agree the thread gauge method, dimensional checks, lot marking and packing details. Confirm how nonconforming product is contained and what records accompany repeat batches.
Request a quotation review: send the controlled drawing, annual or batch quantity, material and finish requirements, and any existing inspection criteria. The review can identify tooling assumptions and the checks needed to keep repeat lots consistent.